The integrity of mechanical systems in commercial vehicles relies heavily on the quality of their sealing components. Among these, the high-performance sealing solutions often referred to as a magnet oil seal are critical for preventing lubricant leakage and protecting internal components from external contaminants, ensuring the longevity of the engine and transmission.
In the demanding environment of the automotive and heavy-duty machinery sectors, selecting the right material is paramount. The industry has shifted toward advanced elastomers that can withstand extreme pressures and temperature fluctuations, reducing downtime and maintenance costs for fleet operators globally.
Understanding the technical specifications of a magnet oil seal allows engineers to optimize vehicle performance. By leveraging materials like Nitrile Butadiene Rubber (NBR), these components provide the essential barrier required to maintain hydraulic pressure and prevent mineral oil degradation.
Material Science of the Magnet Oil Seal
The effectiveness of a magnet oil seal is primarily determined by its elastomer composition. Nitrile Butadiene Rubber (NBR) is the gold standard for these applications due to its exceptional resistance to mineral oils, hydraulic fluids, and greases. This material ensures that the seal does not swell or degrade when exposed to aliphatic hydrocarbons, making it ideal for high-stress automotive environments.
Beyond chemical resistance, the mechanical properties of NBR provide high stability and an impressive temperature operating range from -20°С to +120 °С. This thermal resilience, combined with high resistance to pressure and abrasion, ensures that the seal maintains a tight interface even under the rigorous vibrations and heat cycles typical of Mercedes-Benz commercial vehicle engines.
Global Industry Standards and Relevance
In the global automotive supply chain, adherence to OEM specifications is not just a preference but a necessity for safety and efficiency. The use of a standardized magnet oil seal ensures that replacement parts are fully compatible with original equipment, such as the Mercedes-Benz OEM numbers 006 997 71 47 and A 007 997 75 47. This compatibility prevents catastrophic failures that could lead to oil loss and engine seizure.
Industry benchmarks established by ISO and other international bodies emphasize the need for seals that can withstand diluted acids and alkaline solutions without aromatic or chlorinated additives. By meeting these stringent criteria, manufacturers ensure that their sealing solutions can be deployed across various geographical regions, from the humid tropics to arctic climates, without compromising performance.
The challenge modern industry faces is the balance between cost-efficiency and extreme durability. High-quality sealing components reduce the frequency of repair kits and gasket replacements, which aligns with global efforts to reduce waste and improve the operational uptime of logistics and transport networks.
Core Functional Components and Durability
The architecture of a magnet oil seal is designed to create a leak-proof barrier between a rotating shaft and a stationary housing. The primary goal is to keep the lubricating oil inside the system while preventing dust, water, and debris from entering, which would otherwise accelerate wear on the internal bearings and gears.
Durability in a magnet oil seal is achieved through the synergy of the NBR rubber's abrasion resistance and the precise fitment of the seal's lip. This ensures that the seal can handle the high-pressure environments of commercial vehicle transmissions without developing premature leaks, which is critical for maintaining system pressure.
Furthermore, the stability of the material across a broad temperature spectrum means that the magnet oil seal does not become brittle in cold starts nor lose its elasticity during peak operating temperatures. This consistency is what allows commercial vehicles to maintain reliability over hundreds of thousands of miles.
Performance Metrics and Comparative Analysis
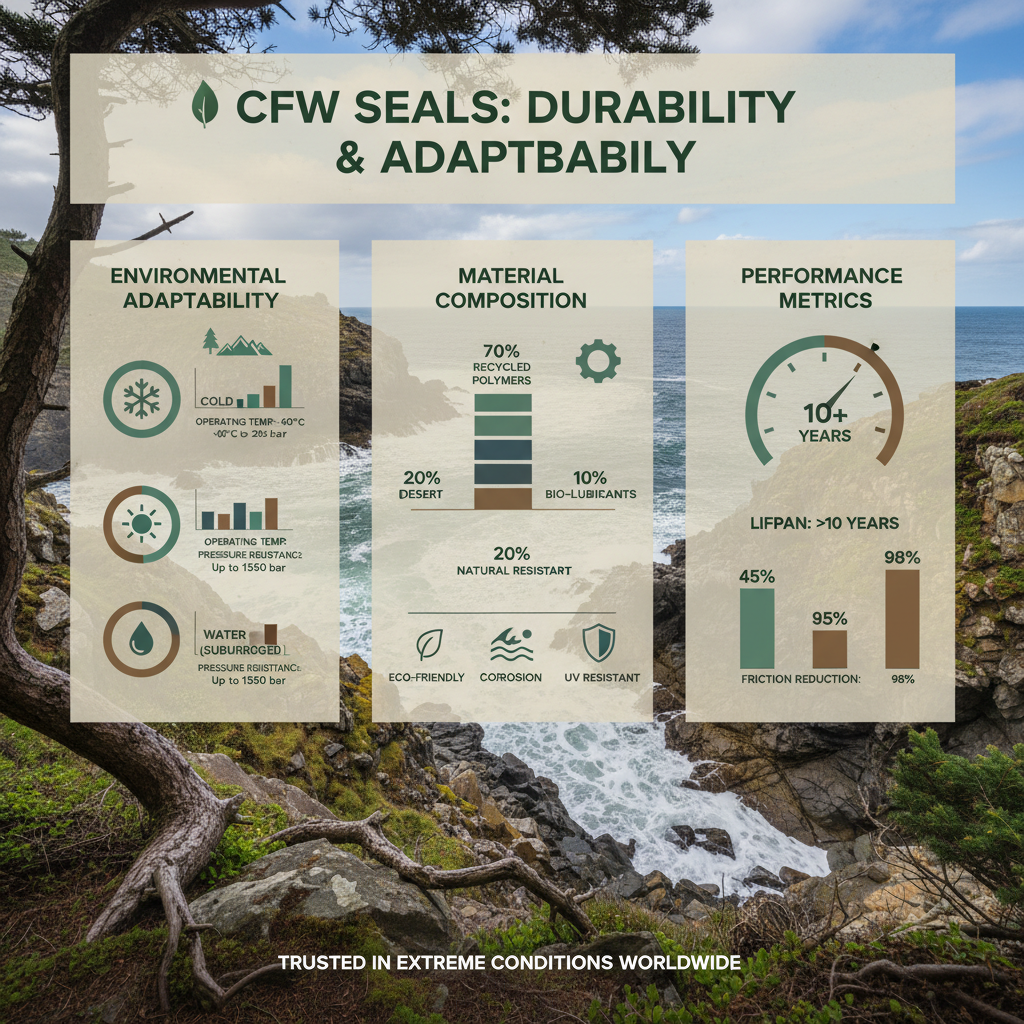
When evaluating the performance of a magnet oil seal, several key metrics are considered: pressure resistance, temperature stability, and chemical compatibility. Different rubber compounds offer varying levels of protection, but NBR remains the most balanced choice for mineral oil applications.
To better understand how these seals perform against different industry requirements, we analyze the ratings of various sealing configurations based on real-world stress tests in commercial transport.
Magnet Oil Seal Performance Analysis
Real-World Applications in Commercial Vehicles
The application of a magnet oil seal is most prominent in the heavy-duty sector, specifically within Mercedes-Benz truck and bus series. These vehicles operate under immense load, where the seal must prevent oil from leaking out of the crankshaft or transmission axles while keeping grit and road salt from entering the lubrication system.
In remote industrial zones or long-haul logistics routes, the reliability of these seals prevents unplanned vehicle downtime. By utilizing NBR-based seals that are compatible with OEM references like 007 997 48 47, fleet managers can ensure that their vehicles maintain peak efficiency regardless of the operating environment.
Long-Term Value and Sustainability
Investing in a high-quality magnet oil seal provides tangible long-term value by extending the service life of the entire powertrain. When a seal fails, it is not just the cost of the part that matters, but the potential damage to the shaft and the cost of the lost oil, which can lead to expensive engine overhauls.
From a sustainability perspective, durable seals contribute to a reduction in environmental pollution. By eliminating oil leaks, these components prevent hydrocarbons from leaching into the soil and waterways, aligning the automotive aftermarket with modern green energy and environmental protection policies.
Moreover, the use of precision-engineered seals reduces the frequency of replacement. This lowers the demand for raw materials and reduces the carbon footprint associated with the manufacturing and shipping of repair kits and gaskets.
Future Innovations in Sealing Technology
The future of sealing technology is moving toward "smart seals" and advanced composite materials. While NBR remains the workhorse for the magnet oil seal, research is exploring the integration of nano-coatings to further reduce friction and heat generation at the seal lip.
Digital transformation is also playing a role, with the development of predictive maintenance sensors that can detect a seal's degradation before a leak occurs. This shift from reactive to proactive maintenance will revolutionize how commercial vehicle fleets manage their components.
Automation in the manufacturing process is ensuring tighter tolerances and more consistent quality. As we move toward a more automated logistics world, the precision of these seals will be the deciding factor in the reliability of autonomous heavy-duty transport.
Technical Specifications and Compatibility Analysis of Magnet Oil Seals
| OEM Reference |
Material Base |
Temp Range |
Oil Resistance |
| 006 997 71 47 |
NBR Rubber |
-20°C to +120°C |
Excellent |
| A 006 997 71 47 |
NBR Rubber |
-20°C to +120°C |
Excellent |
| 007 997 48 47 |
NBR Rubber |
-20°C to +120°C |
Very High |
| 007 997 75 47 |
NBR Rubber |
-20°C to +120°C |
Very High |
| A 007 997 48 47 |
NBR Rubber |
-20°C to +120°C |
Excellent |
| A 007 997 75 47 |
NBR Rubber |
-20°C to +120°C |
Excellent |
FAQS
Most high-performance seals use Nitrile Butadiene Rubber (NBR). This material is chosen for its exceptional resistance to mineral oils, hydraulic fluids, and greases. It can operate effectively between -20°C and +120°C, providing the necessary durability for heavy-duty automotive applications.
Compatibility is verified through OEM reference numbers. For example, if your part matches OEM numbers such as 006 997 71 47 or A 007 997 75 47, it is designed to meet the original factory specifications for fitment and performance in Mercedes-Benz commercial vehicles.
Yes, the NBR rubber used in these seals is engineered for stability from -20°C up to +120°C. This allows the seal to remain flexible in extreme cold to prevent leaks during startup and maintain its structural integrity under high heat during long-haul operations.
Using a non-resistant material would cause the seal to swell, soften, or crack when exposed to mineral oils and diesel fuels. This leads to immediate leakage, loss of lubrication, and potentially catastrophic failure of the rotating shaft or bearing.
Yes, NBR provides good results when exposed to diluted acids and alkaline solutions, provided they do not contain aromatic or chlorinated additives. This makes the seal versatile for various industrial environments where chemical splashes may occur.
Replacement frequency depends on the vehicle's usage and maintenance schedule. However, it is recommended to inspect seals during every major service. Replacing them as part of a repair kit before they fail prevents expensive unplanned downtime and secondary damage to the engine.
Conclusion
In summary, the magnet oil seal serves as a critical line of defense in the maintenance of commercial vehicle powertrains. By combining the chemical resistance of Nitrile Butadiene Rubber (NBR) with precision OEM fitment, these components ensure that lubrication is maintained and contaminants are excluded. The ability to withstand temperatures from -20°C to +120°C and resist a wide array of mineral oils makes them indispensable for the longevity of heavy-duty machinery.
Looking ahead, the integration of smarter materials and predictive monitoring will further enhance the reliability of sealing systems. For fleet operators and technicians, prioritizing high-quality, OEM-compatible seals is the most effective strategy to reduce operational costs and environmental impact. For premium sealing solutions, visit our website: www.yjmseal.com.




 English
 Afrikaans
 Albanian
 Amharic
 Arabic
 Armenian
 Azerbaijani
 Basque
 Belarusian
 Bengali
 Bosnian
 Bulgarian
 Catalan
 Cebuano
 Corsican
 Croatian
 Czech
 Danish
 Dutch
 Esperanto
 Estonian
 Finnish
 French
 Frisian
 Galician
 Georgian
 German
 Greek
 Gujarati
 Haitian Creole
 Hausa
 Hawaiian
 Hebrew
 Hindi
 Miao
 Hungarian
 Icelandic
 Igbo
 Indonesian
 Irish
 Italian
 Japanese
 Javanese
 Kannada
 Kazakh
 Khmer
 Rwandese
 Korean
 Kurdish
 Kyrgyz
 Lao
 Latin
 Latvian
 Lithuanian
 Luxembourgish
 Macedonian
 Malgashi
 Malay
 Malayalam
 Maltese
 Maori
 Marathi
 Mongolian
 Myanmar
 Nepali
 Norwegian
 Norwegian
 Occitan
 Pashto
 Persian
 Polish
 Portuguese
 Punjabi
 Romanian
 Russian
 Samoan
 Scottish Gaelic
 Serbian
 Sesotho
 Shona
 Sindhi
 Sinhala
 Slovak
 Slovenian
 Somali
 Spanish
 Sundanese
 Swahili
 Swedish
 Tagalog
 Tajik
 Tamil
 Tatar
 Telugu
 Thai
 Turkish
 Turkmen
 Ukrainian
 Urdu
 Uighur
 Uzbek
 Vietnamese
 Welsh
 Bantu
 Yiddish
 Yoruba
 Zulu