The reliability of heavy-duty machinery often hinges on the smallest components, and in the realm of suspension and damping, the efficiency of an oil seal shock absorber is paramount. These specialized sealing units are engineered to maintain fluid integrity while preventing the ingress of abrasive contaminants, ensuring that the damping mechanism operates with precision under extreme stress. Whether in agricultural tractors or construction equipment, the right seal prevents leakage and extends the operational lifespan of the entire system.
Globally, the demand for high-performance sealing solutions has surged as industries push the boundaries of machine capacity and environmental resilience. Standard seals often fail when exposed to the severe debris and thermal fluctuations common in off-highway environments, leading to costly downtime and safety risks. This challenge has necessitated the evolution of complex rotary shaft seals, such as cassette seals, which offer a unitized construction to handle higher shaft runout and misalignment than traditional options.
Understanding the technical nuances of an oil seal shock absorber is essential for engineers and maintenance professionals aiming to optimize equipment uptime. By utilizing advanced polymers like Nitrile (NBR) and Fluorocarbon (FKM) rubber, these components can withstand temperatures ranging from -40°F up to 400°F. This guide explores the technical specifications, installation best practices, and the strategic advantages of employing high-end cassette seals in demanding industrial applications.
Technical Foundations of Oil Seal Shock Absorber Systems
At its core, an oil seal shock absorber system relies on a sophisticated interface between the rotating shaft and the stationary housing. Unlike basic seals, high-performance cassette seals utilize a unitized method of construction where spring-loaded sealing elements ride on a self-contained internal wear sleeve. This design is critical for maintaining a tight seal even when the shaft experiences dynamic runout of up to 0.010", a common occurrence in heavy-duty machinery.
The integration of multiple sealing contact points and excluder lips further enhances the system's ability to keep lubricants in and harsh contaminants out. For soft alloy housings, rubber-covered metal OD casings are employed to provide an improved seal against the bore, compensating for thermal expansion and ensuring that the damping fluid remains contained regardless of the external environmental pressure.
The Architecture of Cassette Seals and Hub Reliability
Cassette seals, often referred to as hub seals, are advanced sealing solutions that far exceed the capabilities of traditional oil seals. Their architecture consists of an integrated unit comprising multiple lip seals, a metal or elastomeric outer case, and an inner wear sleeve. This wear sleeve is the primary line of defense, protecting the actual shaft from wear and tear while providing a precision surface for the sealing lips to engage.
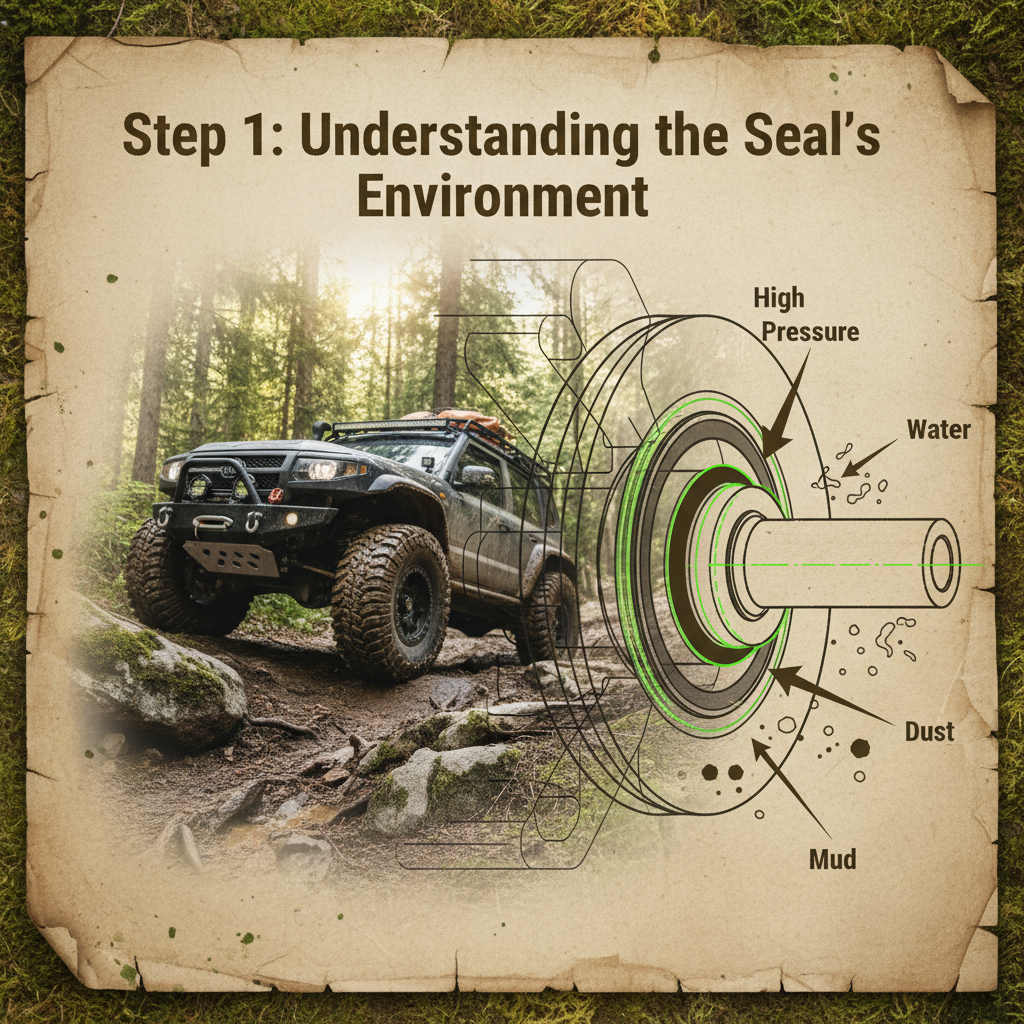
The functional superiority of these seals lies in their labyrinth-like design. By incorporating excluder lips and patented axial face seal surfaces, they can effectively trap and redirect mud, dust, and water away from the internal lubricant. This prevents the "grinding paste" effect, where contaminants mix with oil to erode the shaft and seal, which is a frequent failure point in standard oil seal shock absorber configurations.
Furthermore, these seals are often pre-lubricated with specialized grease. This immediate protection reduces friction during the critical initial startup phase and ensures that the seal is operating at peak efficiency from the moment the machine is powered on. This level of integration makes them indispensable for wheel hubs, axle assemblies, and final drives in off-highway vehicles.
Material Selection for Extreme Operating Environments
Choosing the correct polymer for an oil seal shock absorber is a decision dictated by the temperature and chemical exposure of the application. Nitrile Rubber (NBR and XNBR) is the industry standard for general-purpose applications, providing excellent oil resistance and durability in moderate temperature ranges.
For more extreme conditions, Fluorocarbon Rubber (FKM or FPM) is the preferred choice. When an oil seal shock absorber must operate in high-heat environments, FKM can withstand temperatures up to 400°F (204°C), whereas NBR is typically limited to 250°F. This makes FKM essential for high-performance transmissions and power generation equipment.
Beyond temperature, the casing material also plays a role. Metal casings offer rigid structural support, while rubber-covered metal OD casings provide a softer interface. This is particularly beneficial for housings made of soft alloys, as the rubber cover conforms better to the bore, reducing the risk of leaks caused by thermal contraction or housing imperfections.
Performance Metrics and Operational Limits
The operational efficiency of an oil seal shock absorber is measured by its ability to maintain a seal under varying pressures and speeds. Standard cassette designs typically support a maximum operating pressure of 0 to 7 psi, depending on the shaft speed. The surface speed capacity is impressive, ranging from 2000 to 3200 ft/min (10.2 to 16.3 m/s), allowing them to be used in high-RPM gear reducers and torque hubs.
Another critical metric is the tolerance for misalignment. In real-world heavy-duty applications, shafts are rarely perfectly centered. The ability to handle a maximum shaft-to-bore misalignment of 0.010" ensures that the seal does not fail prematurely due to eccentric rotation, which would otherwise cause uneven wear on the sealing lip.
Performance Rating of Oil Seal Shock Absorber Material Variants
Global Industrial Applications and Use Cases
The implementation of a high-grade oil seal shock absorber is vital across several global industries. In the agricultural sector, tractors operating in muddy fields rely on these seals to prevent soil and water from entering the axle assemblies. Similarly, in the mining industry, where equipment is exposed to abrasive rock dust and extreme loads, the reinforced lip structures of heavy-duty cassette seals ensure that gearboxes remain lubricated and contaminant-free.
Beyond heavy machinery, these seals are used in food processing plants for gear reducers that undergo frequent high-pressure wash-downs. The ability of the seal to resist water spray while maintaining an internal oil barrier is critical for meeting hygiene standards and preventing equipment failure. From remote industrial zones in the Arctic to high-temperature power plants, the versatility of these seals allows for reliable operation in the most challenging terrains on Earth.
Precision Installation for Long-Term Durability
Installing an oil seal shock absorber is a precise operation where a single mistake can lead to premature failure. The process begins with rigorous preparation: the shaft and bore must be thoroughly cleaned of all rust, old sealant, and burrs. Any scoring or eccentricity found on the shaft must be repaired, as the sealing lips are highly sensitive to surface imperfections which can create leak paths.
Lubrication is the next critical step. If the seal is not pre-lubricated, a thin film of compatible grease must be applied to the lips and shaft. Over-lubrication must be avoided to prevent pressure buildup during startup. During the press-fit process, it is imperative to use a guide sleeve or plastic wrap over the shaft edges to avoid nicking the lips, and a proper installation tool should be used to apply force evenly around the outer ring.
The final stage involves verifying the seat and alignment. Once the seal is flush with the housing, the shaft should be rotated by hand to ensure smooth movement. This methodical approach—clean preparation, correct lubrication, and controlled pressing—is what separates a seal that lasts for years from one that fails in weeks.
Future Trends in Advanced Sealing Technology
The future of the oil seal shock absorber is moving toward "intelligent" materials and sustainable manufacturing. We are seeing an increase in the use of low-friction polymers that reduce energy loss and heat generation, which is essential for the next generation of fuel-efficient electric drivetrains and transmissions. These low-friction designs minimize power loss while maintaining the same level of contaminant exclusion.
Digital transformation is also impacting the industry through the use of predictive maintenance. Sensors integrated into the housing near the seal can now monitor temperature and vibration, alerting operators when a seal is approaching the end of its service life. This shifts the maintenance model from reactive to proactive, significantly reducing unplanned downtime in critical infrastructure.
Sustainability is also playing a larger role, with a push toward biodegradable lubricants and recyclable casing materials. As environmental regulations tighten globally, the industry is focusing on seals that not only protect the machine but also protect the environment by eliminating leaks and using eco-friendly materials.
Comparison of Cassette Seal Design Profiles for Shock Absorber Applications
| Design Profile |
Key Feature |
Best Use Case |
Durability Score (1-10) |
| CB Profile |
Metal case with bore sealant |
Standard industrial gearboxes |
8 |
| CL Profile |
Rubber covered OD |
Soft alloy housings |
9 |
| CH Profile |
Enhanced OD sealing |
High-vibration environments |
9 |
| Heavy Duty |
Labyrinth channels |
Mining and Construction |
10 |
| Low-Friction |
Optimized lip geometry |
Electric Vehicle Drivetrains |
7 |
| Custom Design |
Alternate exclusion points |
Extreme misalignment cases |
10 |
FAQS
Cassette seals are unitized components that include an integrated wear sleeve, which protects the shaft from wear. Unlike standard seals, they feature multiple sealing lips and excluders that provide superior protection against mud, water, and dust, making them far more durable in heavy-duty environments where traditional seals would fail due to contamination or shaft runout.
NBR (Nitrile Rubber) is excellent for general oil resistance but is typically limited to temperatures around 250°F. For high-temperature applications, Fluorocarbon Rubber (FKM) is highly recommended, as it can withstand temperatures up to 400°F (204°C) without degrading, ensuring the oil seal shock absorber remains effective under extreme thermal stress.
Standard cassette seal designs generally support operating pressures from 0 to 7 psi. However, the actual pressure limit often depends on the shaft speed. For applications requiring higher pressure resistance, custom-engineered seals with reinforced lip structures and alternate exclusion points can be developed to meet specific operational needs.
To prevent damage, always clean the shaft and bore thoroughly and inspect for burrs. Use a guide sleeve or plastic wrap over the shaft edges to protect the sealing lips during insertion. Most importantly, use a professional press or installation tool to apply force evenly around the outer ring rather than hammering directly on the seal.
Shaft runout refers to the eccentricity or "wobble" of the shaft as it rotates. A high-quality cassette seal is designed to handle a maximum dynamic runout of 0.010", meaning it can maintain a tight seal even if the shaft is not perfectly centered, which is common in large-scale agricultural and construction machinery.
The CL or CH profiles, which feature a rubber-covered metal OD casing, are ideal for soft alloy housings. The rubber covering provides a better seal against the bore by compensating for thermal expansion and housing imperfections, reducing the likelihood of leaks compared to rigid metal casings.
Conclusion
The integration of a high-performance oil seal shock absorber is not merely a maintenance choice but a strategic investment in equipment reliability. By leveraging advanced cassette seal architectures—combining wear sleeves, multiple lip seals, and specialized polymers like FKM and NBR—industries can drastically reduce downtime and protect critical components from the harshest environmental contaminants. From the precision of installation to the selection of the correct design profile, every detail contributes to the longevity of the machine.
Looking forward, the transition toward low-friction materials and predictive maintenance will further refine the efficiency of these sealing systems. As global industries demand higher productivity and lower environmental impact, the evolution of the oil seal shock absorber will continue to be a cornerstone of mechanical engineering. To ensure your equipment operates at its peak, we recommend regular audits of your sealing components and consulting with experts for custom design solutions. Visit our website: www.yjmseal.com


 English
 Afrikaans
 Albanian
 Amharic
 Arabic
 Armenian
 Azerbaijani
 Basque
 Belarusian
 Bengali
 Bosnian
 Bulgarian
 Catalan
 Cebuano
 Corsican
 Croatian
 Czech
 Danish
 Dutch
 Esperanto
 Estonian
 Finnish
 French
 Frisian
 Galician
 Georgian
 German
 Greek
 Gujarati
 Haitian Creole
 Hausa
 Hawaiian
 Hebrew
 Hindi
 Miao
 Hungarian
 Icelandic
 Igbo
 Indonesian
 Irish
 Italian
 Japanese
 Javanese
 Kannada
 Kazakh
 Khmer
 Rwandese
 Korean
 Kurdish
 Kyrgyz
 Lao
 Latin
 Latvian
 Lithuanian
 Luxembourgish
 Macedonian
 Malgashi
 Malay
 Malayalam
 Maltese
 Maori
 Marathi
 Mongolian
 Myanmar
 Nepali
 Norwegian
 Norwegian
 Occitan
 Pashto
 Persian
 Polish
 Portuguese
 Punjabi
 Romanian
 Russian
 Samoan
 Scottish Gaelic
 Serbian
 Sesotho
 Shona
 Sindhi
 Sinhala
 Slovak
 Slovenian
 Somali
 Spanish
 Sundanese
 Swahili
 Swedish
 Tagalog
 Tajik
 Tamil
 Tatar
 Telugu
 Thai
 Turkish
 Turkmen
 Ukrainian
 Urdu
 Uighur
 Uzbek
 Vietnamese
 Welsh
 Bantu
 Yiddish
 Yoruba
 Zulu